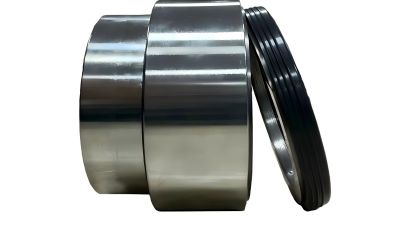
In the fast-paced world of industrial applications, picking the right Chemical Mechanical Seals is more important than ever for buyers around the globe. These seals are pretty much the backbone of maintaining system integrity, stopping leaks, and keeping operations running smoothly. Big names like John Crane, Flowserve, and AESSEAL are always pushing out new and innovative options, so there’s definitely something to fit different needs.
As industries keep evolving, the need for dependable Chemical Mechanical Seals only grows. These parts have to handle tough conditions and harsh chemicals without breaking a sweat. But honestly, choosing the perfect seal isn’t always straightforward — there are so many specs and application requirements to consider. It can be pretty tricky to figure out what’s the best fit, and it really takes some know-how and careful thought.
Getting a good grip on your options and understanding what they really mean in real-world scenarios is key. Manufacturers are always adapting to the latest market trends, but even top-tier products might not tick every box. So, it’s a balancing act — weighing quality against costs. At the end of the day, it’s about thinking through potential limitations and what works best for your specific situation. When you find the right seals, it can lead to better performance and less downtime — which, let’s be honest, we all want.
Overview of Chemical Mechanical Seals in Industrial Applications
Chemical mechanical seals play a crucial role in various industrial applications. These seals are designed to prevent fluid leakage in rotating equipment. Their significance can't be overstated in fields like oil and gas, chemical processing, and wastewater management. The correct application of these seals ensures increased efficiency and safety. They help maintain operational integrity in environments that involve hazardous materials.
Choosing the right seal can be challenging. Factors such as temperature, pressure, and the type of fluid must be considered. Not all seals are created equal. Some may wear out quickly or fail under extreme conditions. Regular maintenance is also vital. Neglecting to check seals can lead to catastrophic failures. Users must remain vigilant and proactive in their maintenance practices.
Innovation continues in the field of mechanical seals. New materials and designs promise enhanced performance and longevity. However, not all advancements will suit every application. Buyers need to evaluate their specific needs carefully. This careful consideration can save costs and ensure reliability in the long run.
Key Features and Benefits of Top Chemical Mechanical Seals
Chemical mechanical seals play a crucial role in various industries, enabling reliable performance in complex systems. They ensure minimal leakage in pumps, particularly in chemical applications. This feature protects the environment and enhances system efficiency. Industry reports suggest that nearly 30% of maintenance costs are linked to seal failures, underscoring their importance.
Key features of top chemical mechanical seals include their material composition and design. Advanced materials like silicon carbide and ceramic increase durability, resisting wear and chemical corrosion. The seal design enhances fluid retention, maintaining pressure stability and prolonging service life. Successful implementation of these seals is heavily reliant on proper installation procedures and routine maintenance.
Tips: Regular inspections can prevent unexpected failures. Ensure that seals are installed according to manufacturer guidelines. It’s wise to review the material compatibility regularly, as changes in fluid composition can affect performance. Investing in high-quality Chemical Pump Mechanical Seals translates into cost savings and improved operational reliability. Remember, the right choice of seal can dramatically influence process efficiency.
2026 Top Chemical Mechanical Seals for Global Buyers Guide
| Seal Type |
Material |
Temperature Range (°C) |
Pressure Range (bar) |
Key Features |
Benefits |
| Single Spring |
PTFE |
-40 to 200 |
0 to 5 |
Simple design, low cost |
Easy to install and replace |
| Double Spring |
Ceramic |
-20 to 150 |
0 to 10 |
Balanced mechanical design |
Reduced leakage and wear |
| Pusher Seal |
Carbon |
-40 to 300 |
0 to 25 |
High flexibility, wider range |
Versatile for various applications |
| Non-Pusher Seal |
Stainless Steel |
-50 to 250 |
0 to 15 |
Minimal maintenance required |
Long service life |
| Cartridge Seal |
Elastomer |
-30 to 150 |
0 to 20 |
Integrated design, easy swap |
Simplifies installation processes |
Material Selection for Chemical Mechanical Seals: A Comprehensive Guide
Material selection is crucial in the production of chemical
Mechanical Seals.
The right material impacts performance and longevity. Various materials, such as elastomers and metal alloys, are used based on application requirements.
For instance, polymers are often suitable for low-pressure applications. However, high-pressure processes may demand stronger, more resilient materials.
Choosing the wrong material can lead to failure in mechanical seals.
This results in leaks and costly downtime.
It is essential to consider chemical compatibility.
Certain materials may degrade in specific environments.
Understanding the operational conditions is vital for ensuring reliability.
Innovations in materials science continually shape seal manufacturing.
New composites and blends offer improved resistance to chemicals and temperature fluctuations.
However, the ideal material depends on the specific application. Proper testing and evaluation are necessary.
Over time, businesses must adapt their strategies to modern challenges.
This reflection on material choice can lead to sustained efficiency in operations.
Major Manufacturers and Their Best-Selling Chemical Mechanical Seals
When it comes to chemical mechanical seals, buyers seek reliability and performance. Many manufacturers specialize in producing these essential components. Each brand has unique offerings tailored to varied industrial applications. Focusing on user needs, they continuously innovate to meet rising demands.
Quality and durability are critical for Chemical Mechanical Seals. Major manufacturers invest in research to ensure optimum performance under extreme conditions. They also frequently update their materials and designs. Nevertheless, some users still report issues with longevity and compatibility. It's vital for buyers to choose seals that match their specific requirements.
Buyers often rely on comparisons and reviews to make informed choices. They should consider factors like application, pressure tolerance, and temperature limits. Even the best products may not suit every situation. Therefore, a thoughtful selection process is crucial for achieving the desired results.
Application Categories: Where Chemical Mechanical Seals Are Used
Chemical mechanical seals are essential in various applications across multiple industries. They serve to prevent leaks and contain fluids effectively, thereby enhancing equipment efficiency. In the chemical processing sector, these seals are critical in reactors and pumps where corrosive substances are handled. Research indicates that up to 30% of maintenance costs can be attributed to seal failures, making robust seal selection crucial.
In the water treatment industry, Mechanical Face Seals play a vital role in pumps and filtration systems. These seals ensure the integrity of systems that handle abrasive and chemically aggressive fluids. A recent industry report highlighted that improper seal choice could lead to equipment downtime of 10-15%. This demonstrates the necessity for reliable sealing solutions.
Moreover, the oil and gas sector relies heavily on chemical mechanical seals to maintain pressure in drilling operations. With the global demand for energy rising, the reliability of these components becomes increasingly important. Statistics indicate that seals can often operate under extreme pressures, yet they require precise installation and selection. Failure to adhere to these can result in costly leaks or even safety hazards. Understanding these applications can guide global buyers in making informed choices for their sealing solutions.
Latest Innovations and Trends in Chemical Mechanical Seal Technology
Chemical mechanical seals are evolving rapidly. In 2026, several trends are shaping this technology. One major innovation is the use of advanced materials. These materials can withstand higher temperatures and pressures. They offer improved resistance to chemical corrosion. This creates longer-lasting seals. The durability of these innovations can reduce maintenance costs significantly.
Another exciting trend is the integration of smart technology. Smart seals can monitor performance in real-time. They can send alerts when leakage occurs. This allows for immediate action, minimizing downtime. Furthermore, the trend towards sustainability is influencing seal design. Manufacturers are focusing on eco-friendly materials. This not only helps the environment but also meets regulatory standards.
However, challenges persist. Some materials may not be universally compatible. This can lead to issues in diverse operating environments. Additionally, the reliance on technology requires proper training for personnel. Misuse of smart features can lead to failures. Travelers in this industry must navigate these complexities carefully.
2026 Top Chemical Mechanical Seals Innovations
Global Market Trends and Forecast for Chemical Mechanical Seals
The global market for chemical mechanical seals is witnessing significant changes. As industries evolve, there is a growing need for high-performance seals. Adaptability and efficiency are key factors driving this market forward. Companies must stay ahead of technology trends to meet customer demands.
Chemical mechanical seals, including Api Mechanical Seals, play a crucial role in various applications. These seals offer reliability in extreme conditions. However, not all manufacturers meet strict quality standards. Buyers should thoroughly evaluate suppliers to ensure long-lasting performance. A lack of stringent quality control may result in costly repairs and downtime.
Emerging technologies are shaping the future of chemical mechanical seals. Smart seals that monitor operational efficiency are on the rise. While this trend is promising, it also presents challenges. Companies need to invest in training and resources to adapt. This shift requires a mindset change, pushing industries to rethink traditional sealing solutions.
Enhancing Industrial Efficiency: The Role of Corrosion-Resistant Mechanical Seals in Pulp Pump Applications - Insights from Recent Market Analysis
In the pulp industry, mechanical seals play a crucial role in maintaining operational efficiency, particularly in environments susceptible to corrosion and clogging. The advent of corrosion-resistant mechanical seals has led to remarkable improvements in the reliability of pulp pump applications. According to recent market analysis, the shift towards enhanced materials and innovative designs has resulted in a significant reduction in maintenance costs and downtime. Industries are increasingly adopting solutions such as single-face balanced configurations, which offer superior performance under challenging conditions.
One noteworthy advancement is the introduction of mechanical seals with features designed specifically to tackle the harsh operating conditions found in pulp processing. For instance, seals equipped with wave springs effectively isolate the process medium, ensuring the prevention of clogging and maintaining a stable performance. Such designs not only enhance the reliability of the pumps but also contribute to overall productivity in factories. Data from industry reports indicate that factories employing these advanced seals have experienced an increase in operational integrity, which directly correlates to improved product output.
The versatility of these modern mechanical seals also allows for a tailored approach to various industrial applications, providing manufacturers with a range of material options. This adaptability is essential for meeting the diverse needs of the pulp industry, thereby driving efficiency and ensuring that operations can proceed uninterrupted. As companies continue to invest in corrosion-resistant technologies, the future of pulp processing looks promising, with mechanical seals poised to play an even more critical role in enhancing industrial efficiency.
FAQS
: Material selection affects performance and longevity. The right choice can prevent leaks and maintain efficiency.
Common materials include elastomers and metal alloys. Polymers suit low-pressure needs, while high-pressure requires stronger options.
Choosing incorrect materials can lead to failures. This often results in leaks and costly downtime for operations.
Understanding conditions is crucial. Specific environments can degrade certain materials, affecting reliability and performance.
They prevent leaks and contain fluids effectively. This enhances equipment efficiency across sectors like chemical processing and water treatment.
Improper choices can lead to downtime. Research shows maintenance costs may rise significantly due to seal failures.
Industries are evolving. There is a growing demand for high-performance seals, driving improvements and adaptability in the market.
Evaluate quality standards of manufacturers. Poor quality can lead to costly repairs and operational disruptions.
Yes, smart seals monitoring efficiency are emerging. They require companies to invest in training and adapt to new demands.
New technologies require a mindset change. Industries must rethink traditional sealing solutions to maintain competitiveness.
Conclusion
The article "2026 Top Chemical Mechanical Seals for Global Buyers Guide" provides a comprehensive overview of Chemical Mechanical Seals (CMS) and their significant role in various industrial applications. It highlights key features and benefits of top CMS, including durability and efficiency, while also offering a detailed guide on material selection for optimal performance. The article categorizes diverse application areas where CMS are essential and discusses the latest innovations and trends shaping their technology. Furthermore, it examines global market trends and offers forecasts for the future of Chemical Mechanical Seals, making it a valuable resource for buyers seeking to understand this critical component of industrial processes.